The importance of dewpoint measurement…
in Welding Gases
Superior weld integrity depends on stringent environmental control. Even parts-per-million (ppm) levels of moisture present in shielding gases, carrier lines, or base materials can introduce critical defects that compromise mechanical strength, surface finish, and long-term durability.
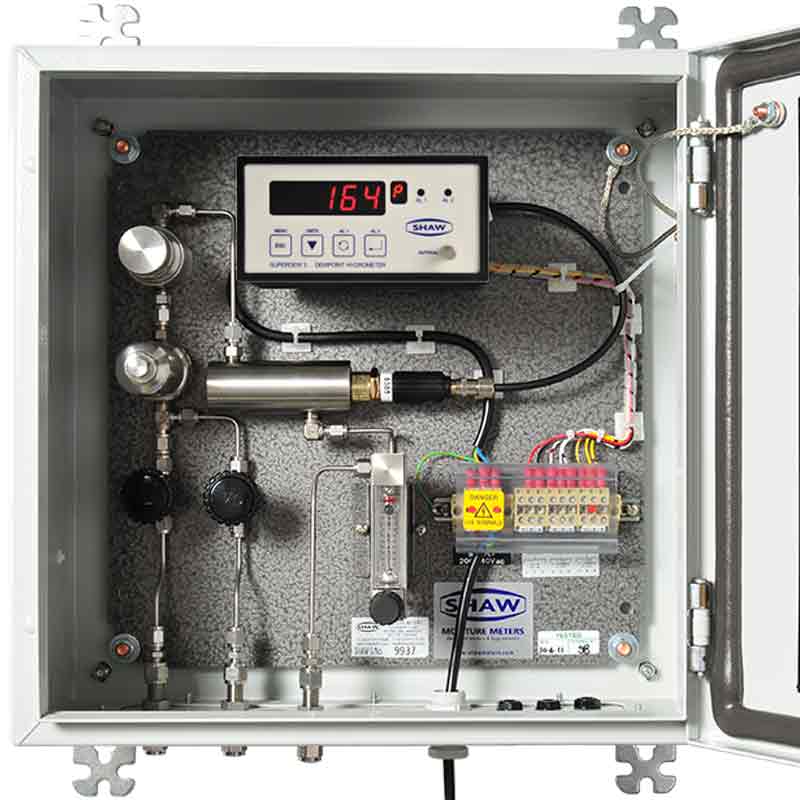
The ability to detect trace moisture at ppm levels enables precise parameter control across welding processes including GMAW (MIG/MAG), GTAW (TIG), laser welding, and other fusion techniques. By integrating reliable Aluminium oxide moisture measurement sensor technologies into gas supply lines or storage vessels, manufacturers can identify moisture ingress before defects arise, ensuring repeatable quality, regulatory compliance, and measurable reductions in scrap and rework.
Understanding Welding Processes
Welding is a foundational fabrication process used to create permanent joints between materials, primarily metals or thermoplastics. It achieves this by applying heat, pressure, or a combination of both, allowing base materials to melt and fuse into a single, unified structure.
What distinguishes welding from mechanical fastening is the fusion mechanism itself, where base materials melt—often with filler material—to form the joint. The resulting bond is permanent and inseparable, unlike bolted or riveted assemblies. Atmospheric protection is also critical; shielding gases or flux are used to prevent contamination of the molten weld pool by oxygen, nitrogen, or moisture.
This process underpins virtually every major industrial sector, including aerospace, automotive, energy, construction, and advanced manufacturing, where structural integrity and load-bearing performance remain uncompromising requirements.
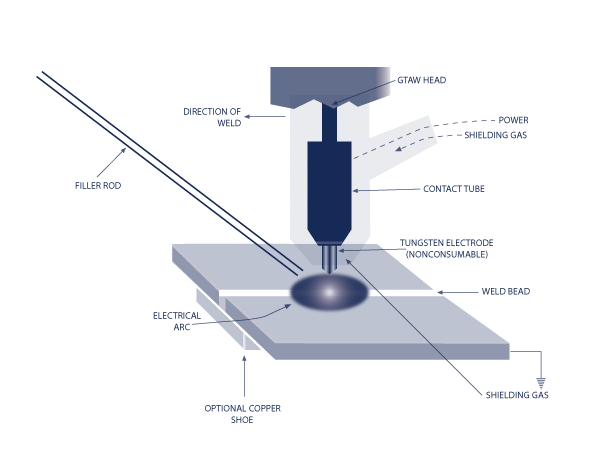
The Critical Role of Welding Gases
Industrial gases such as argon, carbon dioxide (CO₂), helium, oxygen, acetylene, propane, natural gas, and customised blends are indispensable across welding techniques including MIG/MAG, TIG, plasma, laser, and oxy-fuel welding. Their function extends beyond simple shielding.
Shielding gases isolate the weld pool from atmospheric contamination, ensuring metallurgical purity. They stabilise the welding arc to maintain consistent electrical characteristics and uniform penetration. In oxy-fuel systems, gases also act as a fuel source, producing flame temperatures exceeding 3,000 °C.
Gas purity is therefore a decisive factor in weld quality. Even trace contamination—particularly moisture—can disrupt weld chemistry and compromise performance.
How Trace Moisture Introduces Hydrogen
Moisture can enter welding systems through several routes, including ambient humidity, degraded gas lines, and improperly stored electrodes or filler materials. At arc temperatures exceeding 5,000 °C, water vapour (H₂O) dissociates into hydrogen atoms, which dissolve readily into the molten weld pool.
Even at ppm-level concentrations, this significantly increases diffusible hydrogen content. Crucially, hydrogen remains within the material after solidification, leading to delayed weld failures.
Resulting Weld Defects and Structural Risks
The presence of hydrogen derived from moisture initiates a cascade of defects that directly impact weld integrity.
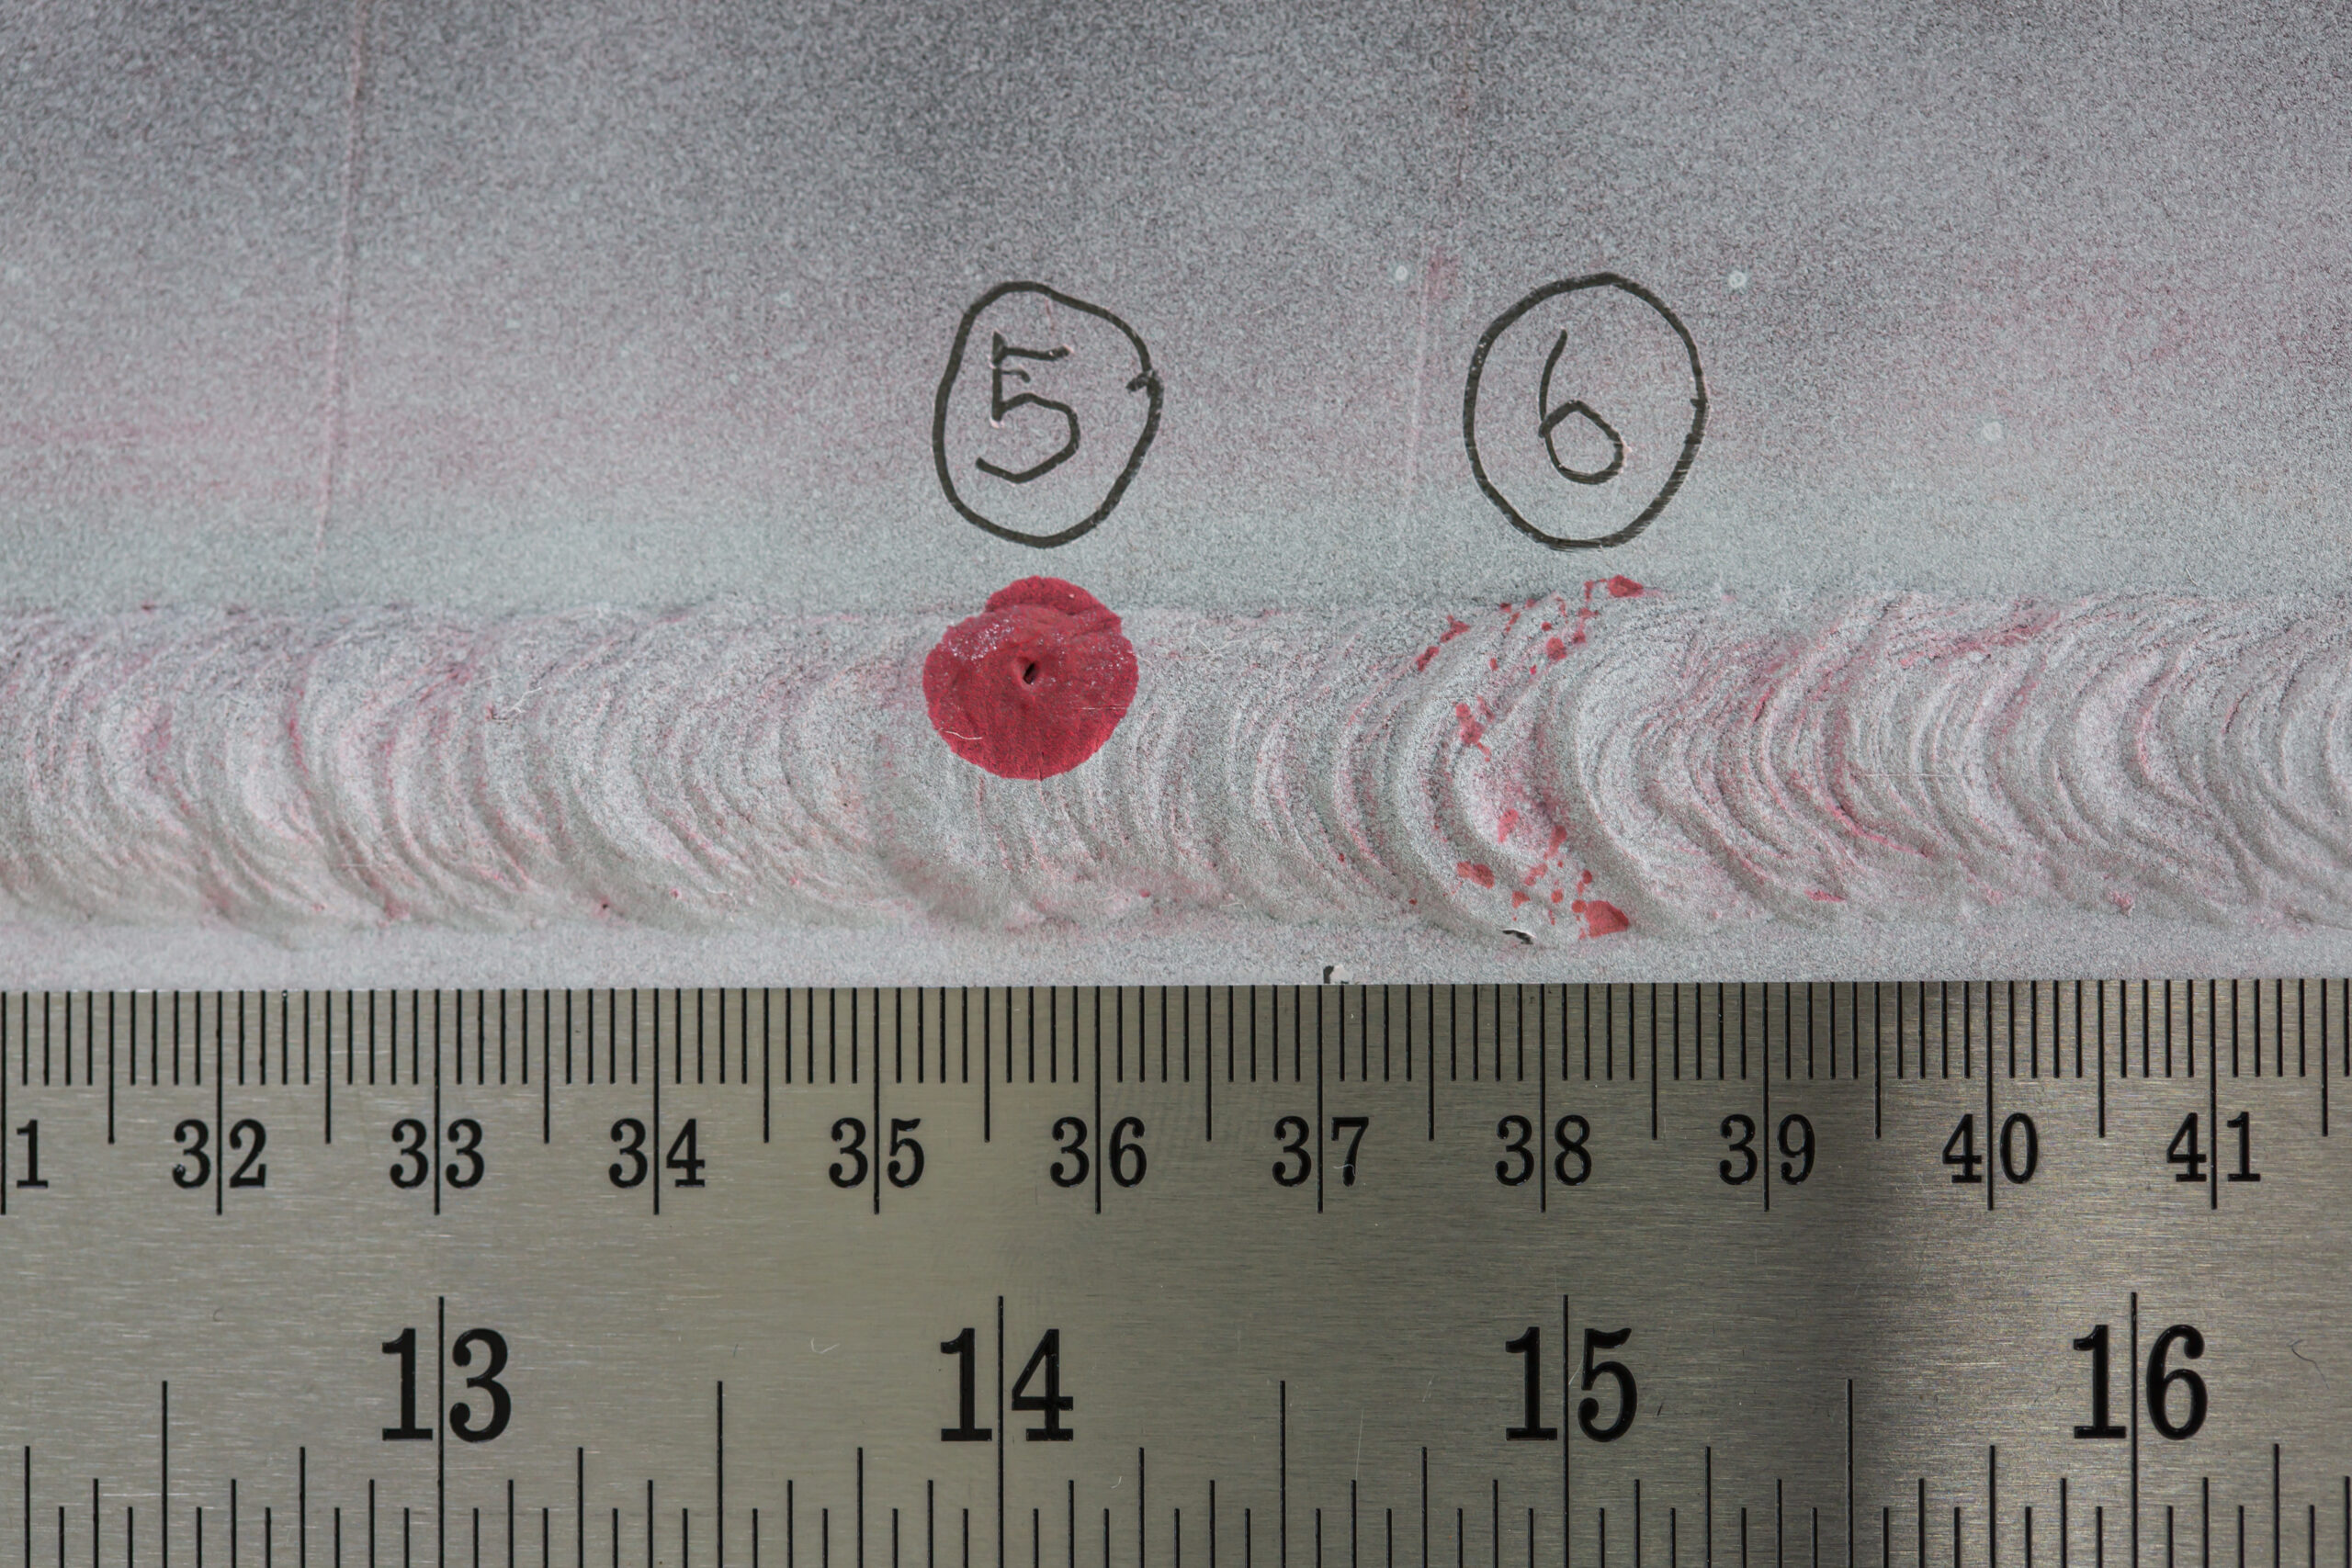
Porosity forms as trapped gas evolves during cooling, producing voids that can reduce cross-sectional strength by more than 50%. Hydrogen embrittlement leads to cold cracking, particularly in high-tensile steels and alloys, often occurring 24 to 48 hours after welding has been completed. This introduces significant safety risks. Additionally, welds become brittle, losing ductility under impact or cyclic loading, and may fail without warning.
Beyond internal defects, visible quality issues also emerge. Irregular weld beads, excessive spatter, and inclusions degrade both the aesthetics and structural performance of the weld. These flaws create stress concentrations that accelerate fatigue failure, especially in dynamic or vibration-heavy environments.
Shielding Gas Instability Caused by Moisture
Moisture contamination can also alter shielding gas chemistry, leading to the formation of reactive compounds such as oxides or hydrides. This destabilises the welding arc and introduces process variability.
Consequences include erratic arc behaviour, inconsistent arc length, and poor penetration control. Oxidation and nitridation effects may increase, particularly on the root side of the weld. TIG welding processes are especially sensitive to these variations, amplifying defect risks.
Moisture Ingress: Sources and Risk Points
Moisture contamination can originate from multiple locations within the gas handling system. Gas cylinders and supply systems may contain intrinsic impurities or experience leaks at valves and changeover points. Hoses and piping are particularly vulnerable, with permeation rates in rubber being significantly higher than in PTFE. Condensation within uninsulated lines further increases risk.
Regulators and filtration systems can introduce moisture through backflow of humid air or saturated filter elements. Additionally, cylinder surfaces and base materials can absorb moisture, which may condense during rapid pressure changes.
Proven Strategies for Moisture Control
Mitigating the risks associated with trace moisture requires a systematic and controlled approach throughout the gas delivery system.
Gas lines should be thoroughly purged using dry argon or nitrogen, with moisture levels verified below 10 ppm(v) before welding begins. Upstream purification using molecular sieve or desiccant dryers provides an additional safeguard against contamination. Gas flow optimisation is equally important; flow rates that are too high can introduce turbulence and entrain ambient air, while insufficient flow compromises shielding effectiveness.
Routine maintenance is essential. This includes quarterly inspection of hoses—preferably constructed from polyurethane or PTFE—along with filter replacement and leak detection using appropriate testing methods. Consumables should be stored in controlled environments such as dry nitrogen cabinets to prevent moisture ingress
Applicable Standards
Industry standards reinforce the importance of moisture control in welding operations. ISO 14175 classifies shielding gases and defines dewpoint limits, such as a maximum of -40 °C dewpoint for certain classifications. In aerospace applications, NADCAP requirements mandate real-time gas purity monitoring in accordance with AC7109 audit criteria. Compliance with these standards demonstrates robust process control and effective risk mitigation.
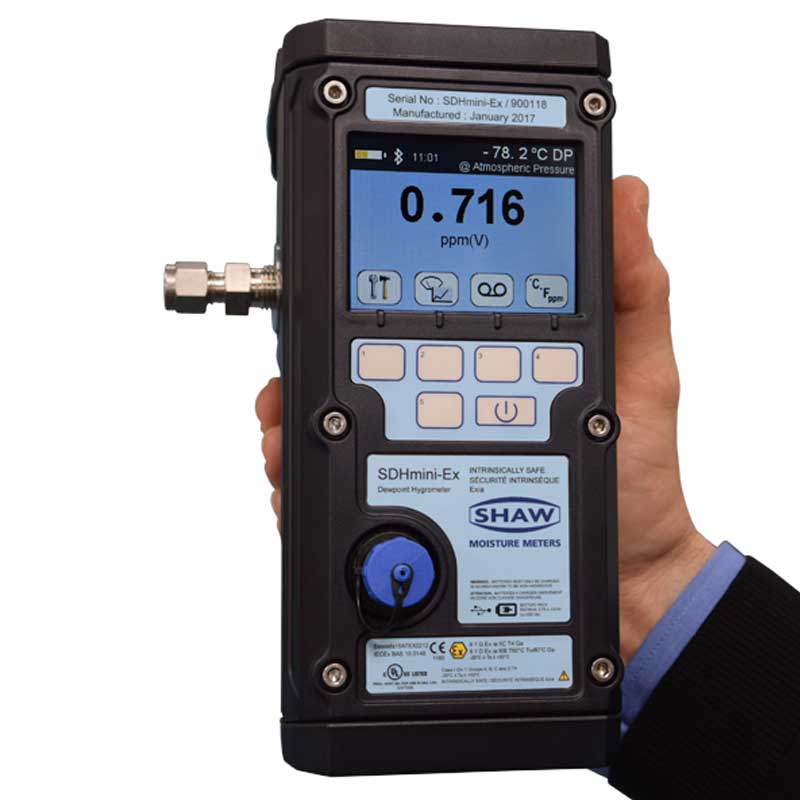
Hand Held Hygrometers
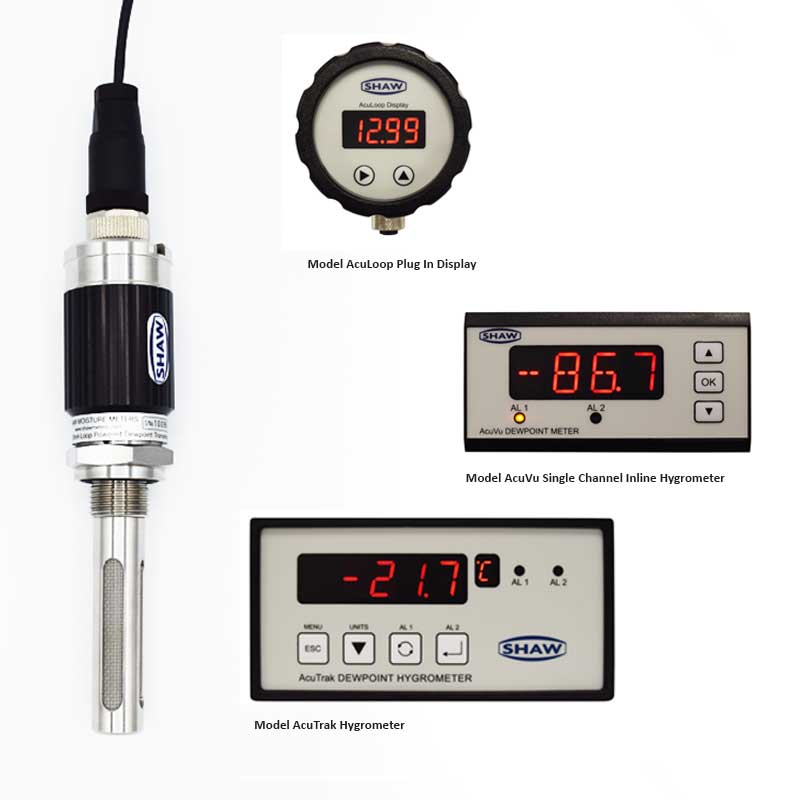
Inline Analyzers